As AI data centers move toward higher computing density, liquid cooling, heavier server systems, and more integrated infrastructure, the aluminum components supporting these systems must meet increasingly demanding requirements.
An aluminum component may look simple, but its performance can depend on many characteristics that are not immediately visible.
A structural profile may require controlled dimensions and straightness.
A CNC-machined cold plate may require precise flatness and sealing surfaces.
A cooling manifold may require accurate port positions and reliable leak performance.
A server chassis may need to maintain dimensional stability while supporting heavy computing hardware.
This makes quality control an essential part of aluminum component quality control for AI data centers.
Quality control should not be limited to checking the finished appearance.
A reliable inspection system should cover the entire manufacturing chain:
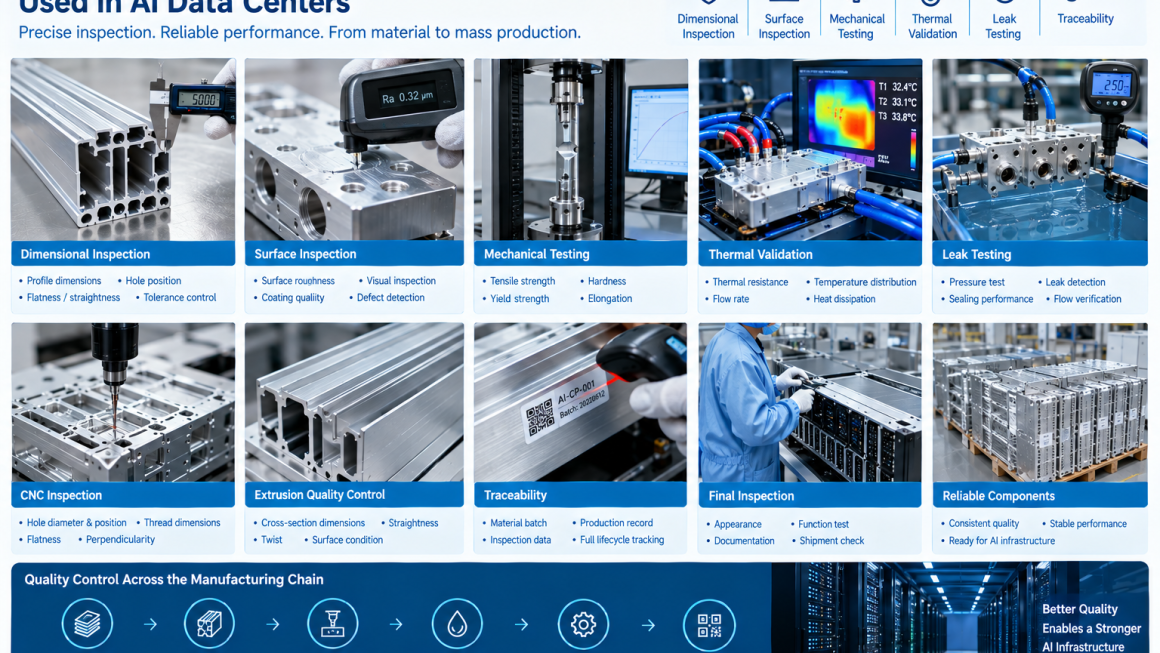
Material → Extrusion → CNC Machining → Surface Treatment → Assembly → Functional Testing → Traceability
The objective is simple:
Every production component should meet the requirements defined for its intended function.
Why Quality Control Matters for AI Infrastructure Aluminum Components
AI infrastructure operates as an interconnected system.
A small dimensional variation in one component can affect another component downstream.
For example:
- A mounting-hole error can affect server assembly.
- A flatness issue can affect a thermal interface.
- A port-position error can increase hose stress.
- A sealing-groove variation can increase leakage risk.
- A profile deformation can affect rack alignment.
- A surface defect can become a corrosion initiation point.
This means quality control should consider both individual component quality and system-level function.
For AI infrastructure aluminum components, the most important quality categories typically include:
- Material verification
- Dimensional inspection
- Surface inspection
- Mechanical testing
- Thermal validation
- Pressure and leak testing
- Surface-treatment inspection
- Cleaning and contamination control
- Traceability
- Final inspection and documentation
Not every component requires every test.
The inspection plan should be based on the actual engineering function of the part.
Quality Control Should Start With the Material
Quality control begins before extrusion or machining.
The incoming aluminum material should be verified against the specified requirements.
Typical material information may include:
- Aluminum alloy
- Temper
- Chemical composition
- Mechanical properties
- Material certificate
- Heat or batch number
- Supplier information
- Raw material dimensions
For common AI infrastructure applications, alloys such as 6061 and 6063 may be considered depending on the structural, thermal, extrusion, and machining requirements.
The important point is not simply to specify an aluminum grade.
The material actually entering production should be traceable to the specified grade and condition.
Material Traceability
Traceability becomes increasingly important as production volume increases.
A production system should ideally allow a finished component to be connected back to:
Finished Part → Production Batch → Manufacturing Process → Raw Material Batch
For example, a production record may include:
- Material batch
- Extrusion production date
- Extrusion profile
- CNC machine
- CNC program revision
- Surface-treatment batch
- Inspection record
- Functional test result
- Final shipment batch
This provides a manufacturing history for the component.
If a quality issue appears later, traceability makes it easier to identify potentially affected production batches.
Dimensional Inspection of Aluminum Components
Dimensional inspection is one of the most fundamental forms of quality control.
For AI data center components, dimensional requirements may include:
- Overall length
- Width
- Height
- Wall thickness
- Hole diameter
- Hole position
- Thread dimensions
- Flatness
- Parallelism
- Perpendicularity
- Straightness
- Profile geometry
The appropriate measurement method depends on the feature.
Simple dimensions may be checked using:
- Calipers
- Micrometers
- Height gauges
- Go/no-go gauges
More complex components may require:
- Coordinate Measuring Machines (CMM)
- Optical measurement
- Vision systems
- 3D scanning
The goal is not to measure every dimension with maximum precision.
The goal is to reliably verify the dimensions that affect component function.
Extrusion Quality Control
Extruded aluminum profiles have their own quality-control requirements.
The extrusion process can influence:
- Cross-sectional dimensions
- Wall thickness
- Straightness
- Twist
- Surface condition
- Cut length
- Internal cavities
- Profile symmetry
For AI infrastructure profiles, inspection may focus on the dimensions that determine:
- Rack alignment
- Structural assembly
- Cooling-channel geometry
- Mounting interfaces
- Cable routing
- Connection with CNC-machined components
A profile can be dimensionally acceptable overall while still having a local feature that creates an assembly problem.
Therefore, inspection should focus on functional interfaces as well as general profile dimensions.
Extrusion Profile Straightness and Twist
Long aluminum profiles can experience dimensional variation during production and handling.
Straightness and twist are particularly important for:
- Server rack frames
- Structural beams
- Mounting rails
- Long cooling channels
- Chassis profiles
A profile that is slightly distorted may become difficult to assemble with other precision components.
For this reason, straightness and twist should be included in the inspection plan when they are functionally important.
CNC Inspection for AI Components
CNC machining introduces another set of quality characteristics.
Typical CNC inspection may include:
- Hole location
- Hole diameter
- Thread dimensions
- Pocket dimensions
- Flatness
- Surface roughness
- Parallelism
- Perpendicularity
- Alignment features
For a CNC-machined aluminum manifold, for example, the inspection may focus on:
- Port position
- Port diameter
- Thread dimensions
- Sealing surfaces
- Mounting-hole pattern
For a cold plate:
- Overall dimensions
- Thermal contact surface
- Channel geometry
- Port location
- O-ring grooves
- Mounting interfaces
This is why CNC inspection should be linked directly to the functional requirements of the component.
Flatness Inspection for Thermal Components
Flatness can be particularly important for AI cooling components.
Examples include:
- Cold plates
- Heat spreaders
- Heat sink bases
- Thermal mounting plates
A flat thermal interface helps maintain consistent contact with the mating surface and thermal interface material.
However, the required flatness should be determined by the thermal design.
Over-specifying flatness can increase machining cost without providing meaningful system-level benefits.
A practical quality-control system therefore asks:
What level of flatness is required for the thermal interface to perform as designed?
Surface Inspection
Surface inspection is not simply about appearance.
For aluminum AI infrastructure components, surface quality can affect:
- Corrosion resistance
- Sealing
- Thermal interfaces
- Assembly
- Surface treatment
- Cleanliness
- Long-term durability
Visual inspection may identify:
- Scratches
- Dents
- Cracks
- Burrs
- Tool marks
- Discoloration
- Surface contamination
For precision components, surface roughness may also need to be measured.
This can be particularly important for:
- Sealing surfaces
- Thermal contact surfaces
- Sliding interfaces
- Precision mounting surfaces
Burr and Edge Inspection
CNC-machined aluminum parts can contain burrs after drilling, milling, and tapping.
Burrs may create problems during assembly or operation.
Potential risks include:
- Damaged seals
- Contamination
- Poor fit
- Cut hazards during assembly
- Restricted fluid passages
- Particle generation
Therefore, deburring should be treated as a defined manufacturing step rather than an informal finishing operation.
Critical internal cooling passages may require additional cleaning and inspection.
Surface Treatment Quality Control
Many aluminum components used in AI infrastructure require surface treatment.
Common processes include:
- Anodizing
- Powder coating
- Conversion coating
- Protective coatings
Quality control may include:
- Coating thickness
- Surface appearance
- Color consistency where applicable
- Adhesion
- Corrosion resistance
- Masking quality
- Dimensional effects
Surface treatment can change the dimensions of precision features.
This is especially relevant for:
- Threads
- Holes
- Sealing surfaces
- Sliding interfaces
- Connector interfaces
The manufacturing process should therefore consider surface treatment together with dimensional inspection.
Mechanical Testing of Aluminum Components
Not every component requires destructive mechanical testing.
However, mechanical properties may need to be verified through material certification or periodic testing depending on the application and quality plan.
Relevant characteristics can include:
- Tensile strength
- Yield strength
- Elongation
- Hardness
For structural AI infrastructure components, mechanical properties are important because the component may support:
- Heavy GPU hardware
- Server chassis
- Cooling equipment
- Power systems
- Cable systems
The specific requirements should be established according to the engineering design and applicable standards.
Structural Load Validation
For critical structural components, dimensional inspection alone may not be enough.
Physical validation may include:
- Static load testing
- Deflection measurement
- Fastener testing
- Vibration testing
- Structural fatigue testing
For example, an aluminum server rack structure may be designed using simulation, but physical testing can provide additional evidence that the actual manufactured structure performs as expected.
This creates an important relationship:
Simulation → Prototype → Physical Validation → Production Control
Quality control should help maintain the characteristics that were validated during development.
Thermal Validation for AI Cooling Components
Thermal components require specialized validation.
For aluminum cold plates, heat spreaders, and cooling structures, relevant parameters may include:
- Thermal resistance
- Temperature distribution
- Coolant flow
- Pressure drop
- Contact temperature
- Heat dissipation capacity
Thermal validation may be performed using controlled test conditions.
The objective is to confirm that the manufactured component performs consistently with the validated design.
This is particularly important when small manufacturing variations could affect the thermal path.
Dimensional Inspection vs. Thermal Validation
These two forms of quality control answer different questions.
Dimensional inspection asks:
Is the component within the specified geometry?
Thermal validation asks:
Does the component achieve the required thermal performance?
A component can pass dimensional inspection and still have unexpected thermal behavior if other factors are not properly controlled.
For this reason, critical thermal components may require both dimensional control and functional thermal testing.
Pressure Testing of Liquid Cooling Components
Liquid cooling components require additional quality controls.
Components such as:
- Cold plates
- Manifolds
- Cooling channels
- Fluid blocks
- Integrated cooling structures
may need pressure testing.
Pressure testing can help verify that the component can withstand the specified operating or test conditions without unacceptable deformation or leakage.
The exact pressure, duration, and test method should be defined according to the component design and system requirements.
Leak Testing
For liquid cooling systems, leak testing is one of the most important functional checks.
Potential leak locations include:
- Threaded ports
- O-ring grooves
- Gaskets
- End closures
- Machined joints
- Connector interfaces
Leak testing can use different methods depending on the component and production requirements.
The important principle is:
Leak prevention should begin with component design and manufacturing control, not only with final inspection.
Machining accuracy, sealing geometry, surface quality, cleanliness, and assembly all contribute to leak performance.
Cleaning and Contamination Control
AI liquid cooling components can contain internal passages that must remain clean.
Machining may generate:
- Aluminum chips
- Fine particles
- Cutting-fluid residues
- Debris
- Burrs
If these contaminants remain inside the component, they can potentially affect cooling-system operation.
Therefore, production may require:
- Cleaning
- Flushing
- Drying
- Visual inspection
- Particle control
For components with internal coolant passages, cleaning should be treated as part of functional quality control.
Quality Control for Cooling Channels
Cooling-channel quality can influence both thermal and fluid performance.
Important characteristics may include:
- Channel dimensions
- Wall thickness
- Surface condition
- Port geometry
- Internal cleanliness
- Pressure integrity
For extruded cooling channels, cross-sectional geometry should remain within the required range.
For CNC-machined channels, tool-path accuracy and surface condition may also be important.
Galvanic Corrosion and Material Compatibility
AI cooling systems may contain multiple metals.
Examples include:
- Aluminum
- Copper
- Stainless steel
- Brass
- Nickel-plated components
Material compatibility should therefore be considered during quality planning.
Potential factors include:
- Coolant chemistry
- Surface treatment
- Electrical contact
- Temperature
- Fluid exposure
- Fastener materials
Quality control may include verification of specified materials and surface treatments to ensure that the production component matches the validated system design.
Inspection of Aluminum-to-Copper Interfaces
Where aluminum components connect with copper cooling components, particular attention may be required.
Inspection may include:
- Interface dimensions
- Surface condition
- Coating condition
- Fastener specification
- Sealing components
- Material identification
This does not mean every aluminum-copper interface will automatically experience a problem.
Rather, the interface should be controlled according to the system’s corrosion-management strategy.
Statistical Process Control for Production
As production volume increases, inspection can move from individual detection toward process control.
Statistical Process Control (SPC) can be useful for selected critical characteristics.
For example:
- Hole position
- Profile dimension
- Wall thickness
- Flatness
- Port location
Instead of simply asking whether one part passes or fails, process data can be monitored to identify trends.
This may help identify:
- Tool wear
- Process drift
- Machine instability
- Material variation
before a large quantity of nonconforming parts is produced.
First Article Inspection
When a new component enters production, a first article inspection can provide a detailed verification of the manufacturing result.
A first article may be checked against:
- Engineering drawing
- CAD model
- Material specification
- Surface-treatment specification
- Critical dimensions
- Functional requirements
For custom AI infrastructure components, first article inspection is particularly useful because many parts may be non-standard.
Once the first article is approved, the production process can proceed under the defined quality plan.
Sampling vs. 100% Inspection
Not every characteristic needs to be inspected on every component.
A practical inspection strategy may combine:
100% Inspection
For highly critical characteristics where failure could create significant system risk.
Examples may include:
- Leak testing
- Critical sealing features
- Certain dimensional interfaces
Sampling Inspection
For stable, well-controlled characteristics where statistical process control is appropriate.
Periodic Validation
For characteristics such as material properties or certain process conditions.
The correct inspection frequency depends on:
- Risk
- Production volume
- Process capability
- Customer requirements
- Component function
Traceability in AI Infrastructure Manufacturing
Traceability connects quality control with the production history.
A robust traceability system may associate each component with:
- Part number
- Revision
- Material batch
- Extrusion batch
- CNC process
- Machine
- Operator or production station
- Surface-treatment batch
- Inspection results
- Functional test results
- Packaging batch
For larger production programs, barcode or QR-based systems may be used to connect physical components with digital production records.
The level of traceability should match the product’s risk and customer requirements.
Digital Quality Records
Modern manufacturing can combine inspection data with digital production records.
For example:
Part ID → CAD revision → Material batch → CNC program → Inspection data → Test result
This creates a digital history for the component.
Such records can help with:
- Quality investigations
- Customer documentation
- Process improvement
- Engineering changes
- Supplier management
- Warranty analysis
For complex AI infrastructure projects, this level of information can become valuable throughout the product lifecycle.
Quality Control Through the Manufacturing Chain
A strong quality system does not rely on final inspection alone.
A better approach is to control quality at each stage.
1. Incoming Material
Verify alloy, temper, dimensions, and documentation.
2. Extrusion
Control profile geometry, straightness, twist, and surface condition.
3. Cutting
Control length and end condition.
4. CNC Machining
Control critical dimensions, threads, holes, flatness, and interfaces.
5. Deburring and Cleaning
Control burr removal and internal cleanliness.
6. Surface Treatment
Control coating or anodizing characteristics.
7. Assembly
Verify fasteners, seals, connectors, and orientation.
8. Functional Testing
Perform pressure, leak, thermal, flow, or structural testing as required.
9. Final Inspection
Verify critical characteristics and documentation.
10. Packaging and Shipment
Protect finished components against damage and contamination.
Quality Control Matrix for AI Aluminum Components
| Component | Dimensional Inspection | Surface Inspection | Mechanical Testing | Thermal Validation | Leak Testing | Traceability |
|---|---|---|---|---|---|---|
| Structural profile | ✓ | ✓ | As required | — | — | ✓ |
| Server chassis | ✓ | ✓ | ✓ | As required | — | ✓ |
| Cold plate | ✓ | ✓ | As required | ✓ | ✓ | ✓ |
| Cooling manifold | ✓ | ✓ | As required | As required | ✓ | ✓ |
| Heat sink | ✓ | ✓ | As required | ✓ | — | ✓ |
| Mounting bracket | ✓ | ✓ | As required | — | — | ✓ |
| Cooling channel | ✓ | ✓ | As required | ✓ | ✓ | ✓ |
| Aluminum enclosure | ✓ | ✓ | As required | As required | — | ✓ |
The actual inspection plan should always be determined by the component’s engineering requirements and application risk.
Common Quality-Control Mistakes
1. Inspecting Only the Final Product
Final inspection cannot always identify where variation was introduced.
2. Measuring Every Dimension Equally
Critical functional dimensions deserve greater attention.
3. Ignoring Material Traceability
A dimensional inspection cannot confirm whether the correct alloy was used.
4. Treating Surface Quality as Cosmetic
Surface condition can affect sealing, corrosion, and thermal interfaces.
5. Skipping Functional Testing
A component can pass dimensional inspection but fail under pressure or thermal conditions.
6. Not Controlling CNC Tool Wear
Machining dimensions can gradually shift during production.
7. Failing to Control Internal Cleanliness
This is particularly important for liquid cooling components.
8. Changing the Design Without Updating Inspection
Engineering revisions must be reflected in drawings, inspection plans, and production documentation.
Building a Quality Plan for Aluminum AI Components
A practical quality plan can follow several steps.
Step 1 — Identify Critical Functions
Determine whether the component is primarily:
- Structural
- Thermal
- Fluid-handling
- Sealing
- Mounting
- Protective
Step 2 — Identify Critical Characteristics
Define the dimensions and properties that control those functions.
Step 3 — Select Inspection Methods
Choose appropriate tools and methods:
- Calipers
- Micrometers
- CMM
- Optical inspection
- Surface roughness measurement
- Pressure testing
- Leak testing
- Thermal testing
Step 4 — Define Inspection Frequency
Decide which characteristics require:
- 100% inspection
- Sampling
- Periodic validation
Step 5 — Establish Traceability
Connect material, manufacturing, inspection, and testing records.
Step 6 — Monitor Production Trends
Use production data to identify process drift.
Step 7 — Continuously Improve
Use inspection and field data to improve design and manufacturing.
Quality Control From Prototype to Mass Production
Quality requirements should evolve together with the product.
Prototype
Focus on:
- Design verification
- Dimensional fit
- Functional testing
Pilot Production
Focus on:
- Process repeatability
- Tooling
- Inspection methods
- Surface treatment
- Production capability
Mass Production
Focus on:
- Process stability
- Statistical control
- Traceability
- Consistent functional performance
- Continuous improvement
This creates a continuous quality loop:
Design → Prototype → Validation → Pilot Production → Quality Control → Mass Production → Field Feedback → Design Improvement
Why Quality Is a System, Not a Final Inspection
For aluminum components used in AI data centers, quality cannot be reduced to a single inspection report.
A reliable component is the result of multiple controlled processes:
Correct material
↓
Correct geometry
↓
Correct machining
↓
Correct surface treatment
↓
Correct assembly
↓
Correct functional testing
↓
Complete traceability
This system-based approach becomes increasingly important as AI infrastructure becomes more integrated.
As AI data centers move toward higher power density and more sophisticated cooling architectures, aluminum components must provide predictable mechanical, thermal, and fluid-management performance.
That makes aluminum component quality control for AI data centers an important part of the overall engineering process.
A robust quality strategy should combine:
- Material verification
- Dimensional inspection
- Extrusion quality control
- CNC inspection
- Surface inspection
- Mechanical testing
- Thermal validation
- Pressure testing
- Leak testing
- Cleaning and contamination control
- Surface-treatment inspection
- Production traceability
The key principle is that inspection should be driven by function.
A structural component needs reliable dimensional and mechanical performance.
A cold plate needs controlled geometry, thermal performance, and leak integrity.
A manifold needs accurate ports, reliable sealing, and clean internal passages.
A chassis needs dimensional consistency, structural stability, and assembly accuracy.
The objective is not to inspect everything in the same way.
It is to identify what matters for each component and control it consistently throughout production.
For AI infrastructure manufacturers, this creates a quality chain:
Material → Extrusion → CNC Machining → Surface Treatment → Inspection → Functional Validation → Traceability
When this chain is integrated into the manufacturing process from the prototype stage through mass production, aluminum components become easier to qualify, easier to scale, and more reliable as part of the larger AI infrastructure system.
Quality is not the final step after manufacturing.
Quality is built into the manufacturing process from the beginning.